
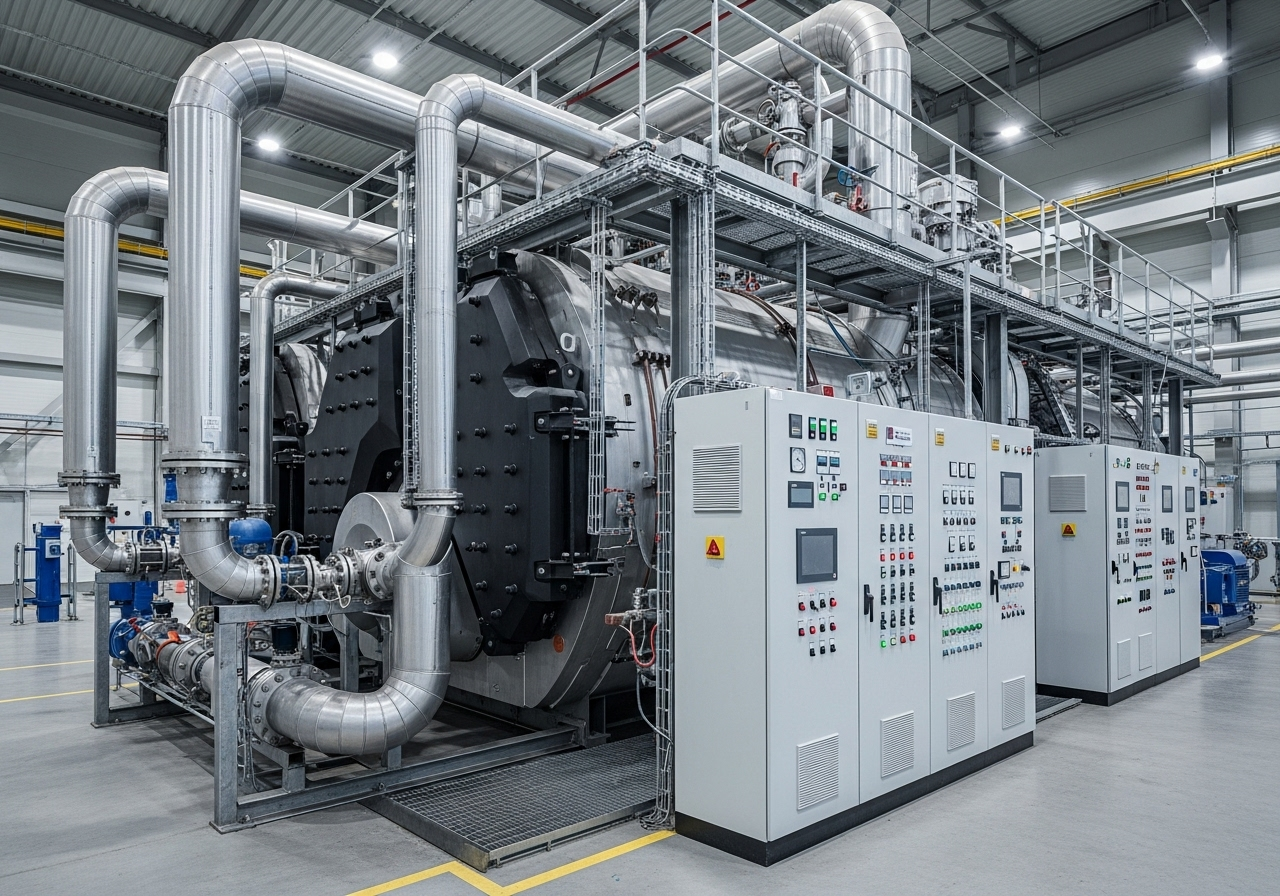
Industrial Steam Boiler Package
High-efficiency industrial boiler systems for power generation and process applications, including waste heat recovery options.
- Engineered to international standards
- Comprehensive quality assurance
- Professional technical support
- Global supply chain capabilities
- Advanced combustion technology for optimal efficiency
- Intelligent control system with remote monitoring
High-efficiency industrial boiler systems for power generation and process applications, including waste heat recovery options. Meritus Technology provides comprehensive industrial solutions, backed by two decades of team experience in China across projects, sourcing and quality. Our Industrial Steam Boiler Package represents the highest quality in boilers & power equipment technology, engineered for demanding applications and backed by worldwide support. Each unit is manufactured to international standards with complete material traceability and certification, ensuring reliable performance in the most challenging industrial environments.
Certifications & Standards
Industries Served
Key Advantages
Preparation Requirements
Site survey and preparation, foundation design, utility connections planning, and permit acquisition for Industrial Steam Boiler Package
Installation Steps
- 1Site preparation and material verification
- 2Foundation work and anchor installation
- 3Equipment positioning and alignment
- 4Utility connections (electrical, pneumatic, hydraulic)
- 5System commissioning and testing
- 6Performance verification and documentation
- 7Operator training and handover
Required Tools & Equipment
Professional installation tools, lifting equipment, welding facilities, testing instruments, and calibration equipment
Safety Requirements
Comprehensive safety protocols including PPE requirements, confined space procedures, electrical safety, and hot work permits
Technical Support
24/7 global technical support hotline with experienced industrial engineers
Field Service
Worldwide service network with certified technicians and rapid response capabilities
Training Programs
Comprehensive operator training and certification programs available globally
Documentation
Complete technical documentation including installation guides, O&M manuals, and maintenance schedules